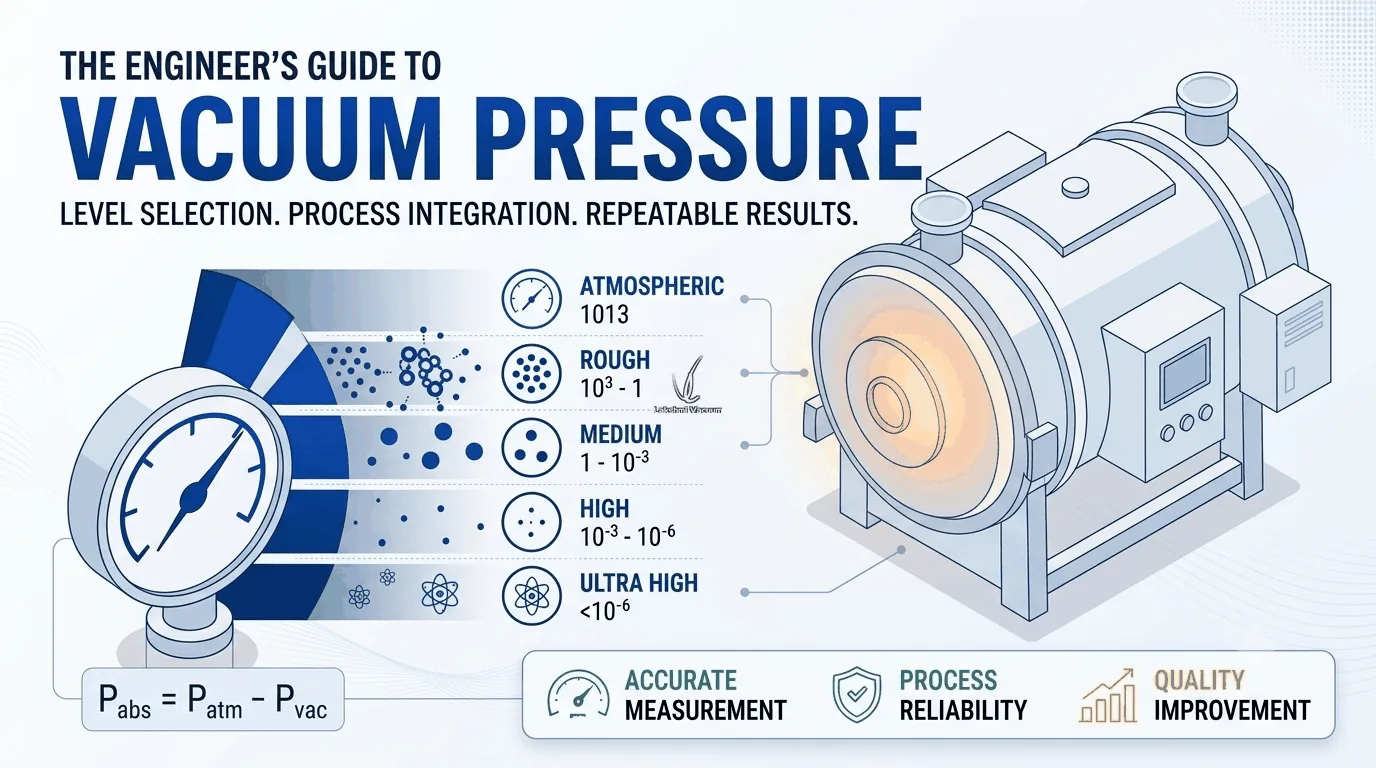
Vacuum heat treatment has revolutionized modern metallurgy, offering unparalleled control over the thermal processing of advanced materials. Unlike conventional atmospheric furnaces, an industrial vacuum furnace removes the environment itself, replacing it with a precisely controlled void. This absence of oxygen prevents oxidation, decarburization, and contamination, ensuring that high-value components emerge with bright, clean surfaces and repeatable metallurgical properties.
1. Understanding Vacuum Pressure Fundamentals
The Core Formulas
- Absolute Pressure (Pabs): Total pressure measured relative to a perfect vacuum (zero).
- Atmospheric Pressure (Patm): ~1013 mbar at sea level.
- Vacuum Pressure: Patm − Pabs. As absolute pressure drops, vacuum increases.
Why It Matters
- Determines the mean free path of gas molecules.
- Dictates the residual gases present (O2, H2O, N2).
- Directly influences surface reactions on the workpiece.
Units of Measurement in Vacuum Engineering
| Unit | Symbol | Value (in Pascals) | Common Usage |
|---|---|---|---|
| Standard Atmosphere | atm | 101,325 Pa | Reference point |
| Bar | bar | 100,000 Pa | Quench pressure (2, 6, 20 bar) |
| Millibar | mbar | 100 Pa | European furnaces, vacuum level |
| Torr | Torr | 133.322 Pa | Legacy/US furnaces |
| Pascal | Pa | 1 Pa | SI Unit (Scientific) |
2. The Spectrum of Vacuum Ranges & Pumping Systems
Rough & Medium Vacuum
10-2 to 10-3 mbar. Achieved with rotary vane, screw, or roots pumps. Ideal for hardening of tool steels, sintering, and degassing.
High Vacuum (HV)
10-4 to 10-6 mbar. Requires oil diffusion or turbomolecular pumps. Used for brazing and for heat treatment of superalloys and titanium.
Ultra-High Vacuum (UHV)
Below 10-7 mbar. Rarely used in standard heat treatment, reserved for aerospace material research and specific semiconductor annealing.
Engineering Insight: Partial Pressure
In vacuum heat treatment, partial pressure is often used. Instead of pulling a deep vacuum continuously, inert gases like argon or nitrogen are intentionally backfilled to a specific pressure (e.g., 1 to 10 mbar) at high temperatures. This prevents the evaporation of alloying elements (like chromium or manganese) from high-alloy tool steels, preserving the metallurgical integrity of the workpiece. Our vacuum hardening furnaces are engineered to handle these precise transitions seamlessly.
3. The Metallurgical Advantage of Vacuum
The Physics of Heat Transfer: In a deep vacuum, convective heat transfer is almost non-existent. Heat is transferred purely by radiation. This means the workpiece only heats up when it "sees" the radiant heating elements. This allows for incredibly uniform temperature distribution, minimizing thermal gradients and the resulting distortion in complex geometries.
Material Compatibility in Vacuum
- Tool Steels (H13, D2, A2): Benefit heavily from vacuum hardening to prevent surface scaling and maintain sharp edges on tooling.
- Stainless Steels (300 & 400 Series): Require vacuum annealing to prevent sensitization (chromium carbide precipitation) which causes intergranular corrosion.
- Superalloys (Inconel, Titanium): Highly reactive at elevated temperatures; vacuum processing is mandatory to prevent alpha-case formation in titanium and oxidation in nickel-based superalloys.
4. The Furnace Selection Framework
- Operating Temperature: Do you need 1100°C for hardening tool steels, or 1600°C for sintering ceramics?
- Vacuum Level: Does your process require 10-4 to 10-6 mbar (High Vacuum) or will medium vacuum suffice?
- Quenching Method: What is the required cooling rate? Gas quenching (N2 or Ar) at 2-bar, 6-bar, or up to 20-bar, or oil?
- Hot Zone Materials: Graphite (cost-effective) vs. All-metal molybdenum/tungsten shields (cleanest, aerospace).
- Throughput & Loading: Workpiece dimensions, total load weight, and required cycle times.
- Cycle Uniformity: Compliance with AMS 2750 standards for temperature uniformity surveys.
Gas Quenching Dynamics
Modern vacuum furnaces predominantly use high-pressure gas quenching rather than oil. The cooling rate is dictated by the gas type, pressure, and fan velocity. If your process involves joining metals, explore our specialized vacuum brazing furnaces.
| Gas Type | Density | Thermal Conductivity | Application |
|---|---|---|---|
| Nitrogen (N2) | Medium | Medium | General purpose, cost-effective |
| Argon (Ar) | High | Low | Reactive materials (Titanium) |
| Helium (He) | Low | High | Ultra-fast cooling (often recovered) |
5. Partnering with a Vacuum Furnace Manufacturer
Selecting the right parameters is only half the battle. The true ROI is realized when you partner with an experienced vacuum furnace manufacturer who understands the nuances of metallurgical process control. Custom engineering is often required to integrate specific pumping capacities, hot zone configurations, and control systems that align with your unique manufacturing workflow.
At Lakshmi Vacuum, we engineer thermal solutions. Whether you are scaling up for aerospace production, automotive transmission hardening, or medical device brazing, our manufacturing capabilities ensure repeatable AMS 2750 compliance. We also offer comprehensive vacuum heat treatment services.
6. Industry Applications
Aerospace
Landing gear components, turbine blades, and structural titanium alloys requiring flawless bright surfaces and strict AMS compliance.
Automotive
High-volume transmission gears, CV joints, and fuel injection components demanding minimal distortion and precise hardness.
Electronics & Medical
Brazing of hermetic seals, semiconductor chamber components, and surgical instruments requiring sterile, flux-free joints.
7. Conclusion
The right vacuum furnace selection starts with understanding pressure fundamentals, then systematically matching process requirements to furnace capabilities. By accurately defining your temperature, vacuum level, and quenching parameters, you ensure optimal metallurgical results, lower operating costs, and decades of reliable thermal processing.
Frequently Asked Questions
The vacuum level depends on the process. Hardening of tool steels and sintering are typically done in the medium vacuum range, while brazing and heat treatment of superalloys and titanium call for high vacuum, typically 10-4 to 10-6 mbar.
Cooling rate is directly tied to gas density. Higher quench gas pressure raises gas density and significantly increases the cooling rate. High-pressure gas quenching (up to 20-bar) can replace oil quenching for certain steel grades.
Yes. As a dedicated vacuum furnace manufacturer, we specialize in custom engineering. From specific hot zone dimensions to integrated material handling systems and advanced PLC controls, we tailor the furnace to your exact production footprint. Request a quote today.
The absence of oxygen means no oxidation occurs, leaving the workpiece with a bright, clean finish that requires no post-treatment machining. It also ensures zero decarburization, preserving surface hardness and fatigue strength.
Ready to Upgrade Your Heat Treatment Capabilities?
Whether you are looking to purchase a new industrial vacuum furnace, upgrade your existing thermal processing line, or need expert consultation on furnace selection, our engineering team is ready to support your manufacturing goals.
Request a Technical Consultation