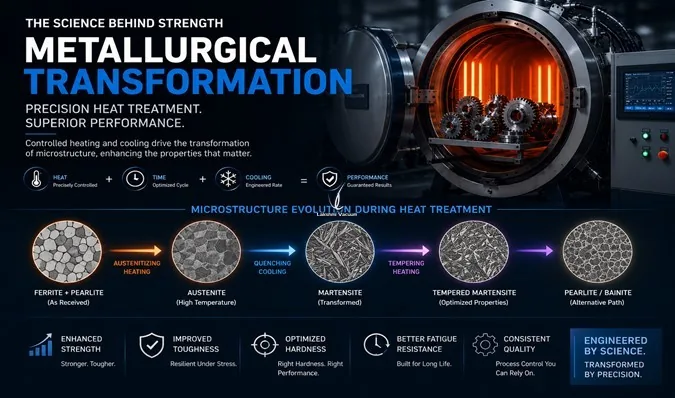
When you pick up a precision aerospace component or a high-performance gear, you aren't just holding a piece of metal. You are holding a snapshot of a thermodynamic battle fought at the atomic level. Whether a gear endures a million cycles or fails catastrophically rarely depends on the steel's chemistry alone. It depends on how the internal structure was manipulated. This is the domain of metallurgical transformations in vacuum heat treatment.
What are Metallurgical Transformations?
Metallurgical transformations in vacuum heat treatment are the deliberate alterations of a metal's internal crystal structure and phase composition, driven by precisely controlled heating and cooling cycles. These transformations rearrange atoms at the microscopic level, directly dictating the mechanical properties of the component, such as hardness, toughness, and ductility.
Understanding Metallurgical Transformations
To master heat treatment, we must stop viewing metal as a static solid and start seeing it as a dynamic system. At room temperature, atoms in steel are locked into a specific arrangement. Introducing thermal energy causes intense vibration, breaking bonds and shifting the structure.
We use this instability to our advantage. Heating steel into the austenitic range transforms it into a face-centered cubic lattice capable of dissolving high amounts of carbon. Slow cooling allows carbon to precipitate out, softening the metal. Rapid cooling traps that carbon inside the lattice, creating immense internal stress and hardness.
Engineering Principle
These phase transformations in steel are predictable physical changes that we exploit to solve complex engineering problems. Controlling the metallurgical transformations in steel vacuum heat treatment process is what allows us to tailor material performance to specific application demands.
Key Phase Transformations
1. Austenite to Martensite
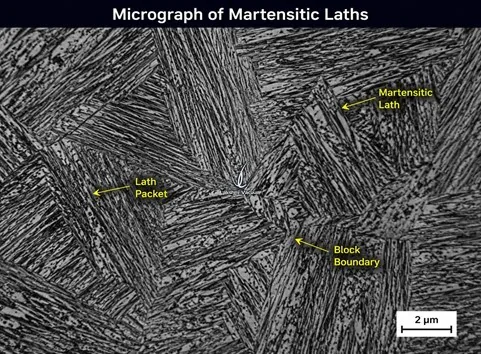
The most critical transformation for hardening. Carbon atoms cannot diffuse out during rapid quenching, creating a body-centered tetragonal structure supersaturated with carbon — extremely hard and brittle.
2. Pearlite Formation
Forms during slow cooling. Carbon precipitates as Iron Carbide (Cementite) alternating with layers of pure Ferrite. Softer and more ductile — ideal for machinability and cold forming.
3. Bainite Transformation
Forms at cooling rates between Pearlite and Martensite, typically requiring isothermal hold. Non-lamellar mixture of ferrite and cementite — balances strength and toughness.
Key Takeaway: The austenite to martensite transformation is the primary mechanism for creating wear-resistant surfaces in tools and bearings.
Microstructure Importance
The resulting microstructure dictates the macro-scale behavior of the part. You cannot specify hardness without considering the microstructure changes during vacuum heat treatment:
Hardness & Strength
A fine-grained Martensitic structure provides superior hardness, resisting deformation. Trapped carbon atoms block dislocation movement within the lattice.
Ductility
Martensite has very low ductility. We must temper it to allow a tiny amount of carbon to precipitate, relieving stress without sacrificing hardness.
Grain Size
Coarse grains act as stress concentrators. A precise thermal cycle prevents excessive grain growth, ensuring isotropic and predictable behavior.
TTT and CCT Diagrams
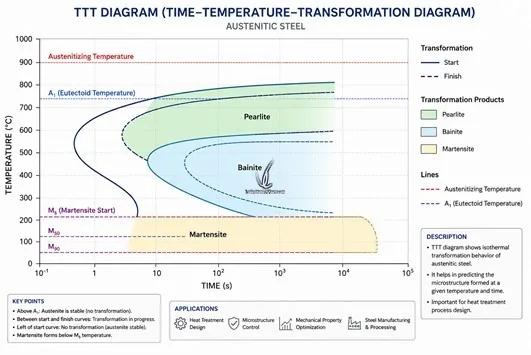
Engineering relies on data, not guesswork. We use Time-Temperature-Transformation (TTT) and Continuous Cooling Transformation (CCT) diagrams to plan our thermal cycles. These are not just academic curves; they are essential tools for process planning.
| Diagram Type | Method | Best For | Industry Use |
|---|---|---|---|
| TTT Diagrams | Constant temperature over time | Isothermal processes | Austempering planning |
| CCT Diagrams | Continuous cooling | Real-world furnace cycles | Full hardening optimization |
Critical Zone: The "nose" of the CCT curve is the critical zone. If the cooling curve cuts through the nose, soft Pearlite forms. If the curve skirts the nose, we achieve full hardening with Martensite formation.
The Role of Vacuum Heat Treatment
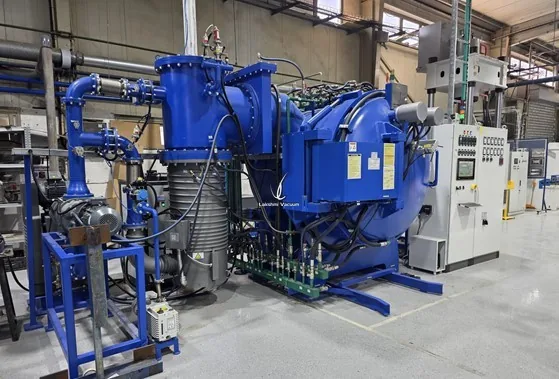
Executing these transformations requires precise control over the atmosphere and temperature. This is where the vacuum heat treatment process proves superior to conventional atmosphere furnaces.
- Oxidation-Free Environment: Atmospheric furnaces introduce surface oxidation and decarburization. Vacuum eliminates reactive gases, ensuring the austenite to martensite transformation occurs uniformly right to the surface.
- Bright Finish: Without oxidation, parts emerge clean and bright. This eliminates post-processing like pickling or blasting, reducing cost and lead time.
- Uniform Heating: Vacuum furnaces use radiant heat transfer, providing exceptional temperature uniformity across complex geometries.
- Controllable Cooling: With gas quenching capabilities, we can precisely tune cooling rates to target specific phases — whether that's full Martensite, Bainite, or a controlled mixed structure.
Industrial Applications
The ability to control metallurgical transformations in steel vacuum heat treatment process has far-reaching implications across industries:
Aerospace
Landing gear components, turbine blades, and fasteners require precise case hardening with minimal distortion — only achievable through vacuum-controlled transformations.
Automotive
Transmission gears, camshafts, and CV joints demand a hard, wear-resistant surface with a tough core — achieved through carburizing followed by controlled quenching.
Tooling & Dies
Mold inserts, stamping dies, and cutting tools require extreme surface hardness. Vacuum hardening ensures uniform Martensite formation without decarburization.
Common Challenges in Controlling Transformations
Even with advanced equipment, several factors can derail the desired phase transformations in steel:
Uneven Heating
Large or complex sections may heat non-uniformly, causing incomplete austenitization and mixed microstructures.
Quench Rate Variability
Insufficient quench speed allows Pearlite to form at the core while the surface achieves Martensite — a dangerous property mismatch.
Distortion
Thermal gradients and phase volume changes (austenite to martensite expands ~4%) cause dimensional changes that may exceed tolerances.
Advanced Transformation Control Techniques
Modern vacuum heat treatment offers sophisticated methods to overcome these challenges:
Austempering
Holding at a temperature in the Bainite region to produce a tough, wear-resistant structure without the brittleness of Martensite. Ideal for springs and impact-loaded components.
Multi-Step Processing
Sub-critical Annealing followed by Hardening. Refines the starting grain structure before the final hardening cycle, resulting in a finer, more uniform Martensitic microstructure with improved toughness.
Quality Verification
Verifying that the intended metallurgical transformations in vacuum heat treatment have occurred correctly requires systematic testing:
- Hardness Testing: Vickers, Rockwell, or Brinell testing at multiple locations to verify uniform transformation across the part.
- Metallographic Examination: Cross-sectional polishing and etching to visually confirm the microstructure matches specifications.
- Case Depth Measurement: For carburized parts, verifying the effective case depth ensures the hard layer meets design requirements.
- Retained Austenite Measurement: X-ray diffraction to quantify any untransformed Austenite that could affect long-term stability.
Conclusion
Understanding and controlling metallurgical transformations in vacuum heat treatment is what separates reliable, high-performance components from unpredictable failures. Every phase transformation — whether Austenite to Martensite, Pearlite formation, or Bainite development — represents a deliberate choice in the engineering of material properties.
At Lakshmi Vacuum, our advanced vacuum furnaces provide the atmospheric purity, temperature uniformity, and quench control necessary to execute these transformations with precision. Whether you need full hardening, case carburizing, or specialized treatments like austempering, our engineering team understands the metallurgy behind every thermal cycle.
Frequently Asked Questions
The austenite to martensite transformation is the most critical. It occurs during rapid quenching when carbon atoms are trapped in the crystal lattice, creating extreme hardness. This transformation is diffusionless — it happens almost instantaneously through a shear mechanism rather than atomic diffusion.
Vacuum eliminates oxygen and other reactive gases, preventing surface oxidation and decarburization. This means the phase transformations in steel occur uniformly right to the surface, producing consistent hardness without a soft, decarburized layer that atmosphere furnaces typically create.
Yes. By programming an isothermal hold at the appropriate temperature (typically 250-400°C depending on the steel grade) after austenitizing, Bainite can be formed. This process, called austempering, produces a structure with excellent toughness and is well-suited to vacuum furnace capabilities.
Retained Austenite occurs when the cooling rate is insufficient or the alloy has high carbon content, preventing complete transformation to Martensite. It can be problematic because it is metastable — it may transform over time, causing dimensional changes. Cryogenic treatment or multiple tempers can convert retained Austenite to Martensite.
Need Expert Vacuum Heat Treatment?
Our metallurgical engineering team can help you select the right thermal cycle for your application and material specification — and put it into production with our vacuum heat treatment services.
Request a Consultation